Vacuum Systems
A twin lobe blower package configured for low-pressure vacuum duties in industrial process systems.
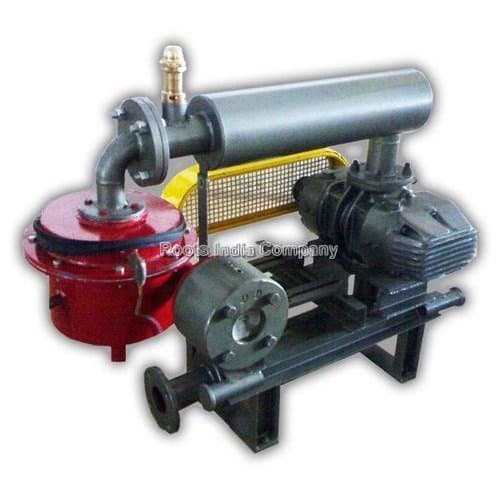
- Continuous air or gas removal
- Stable vacuum-duty performance
- Coordinated inlet protection
- Configurable discharge treatment
Product overview
Built Around the Operating Requirement.
Vacuum-duty twin lobe blowers are considered for applications that need continuous air or gas removal. The complete system should be assessed for suction conditions, filtration, temperature, noise and discharge handling.
Talk to Our TeamTypical applications
Designed for Diverse Industrial Needs.
Representative operating contexts for this equipment category. Final selection depends on the required duty and site conditions.
Representative application
Vacuum conveying
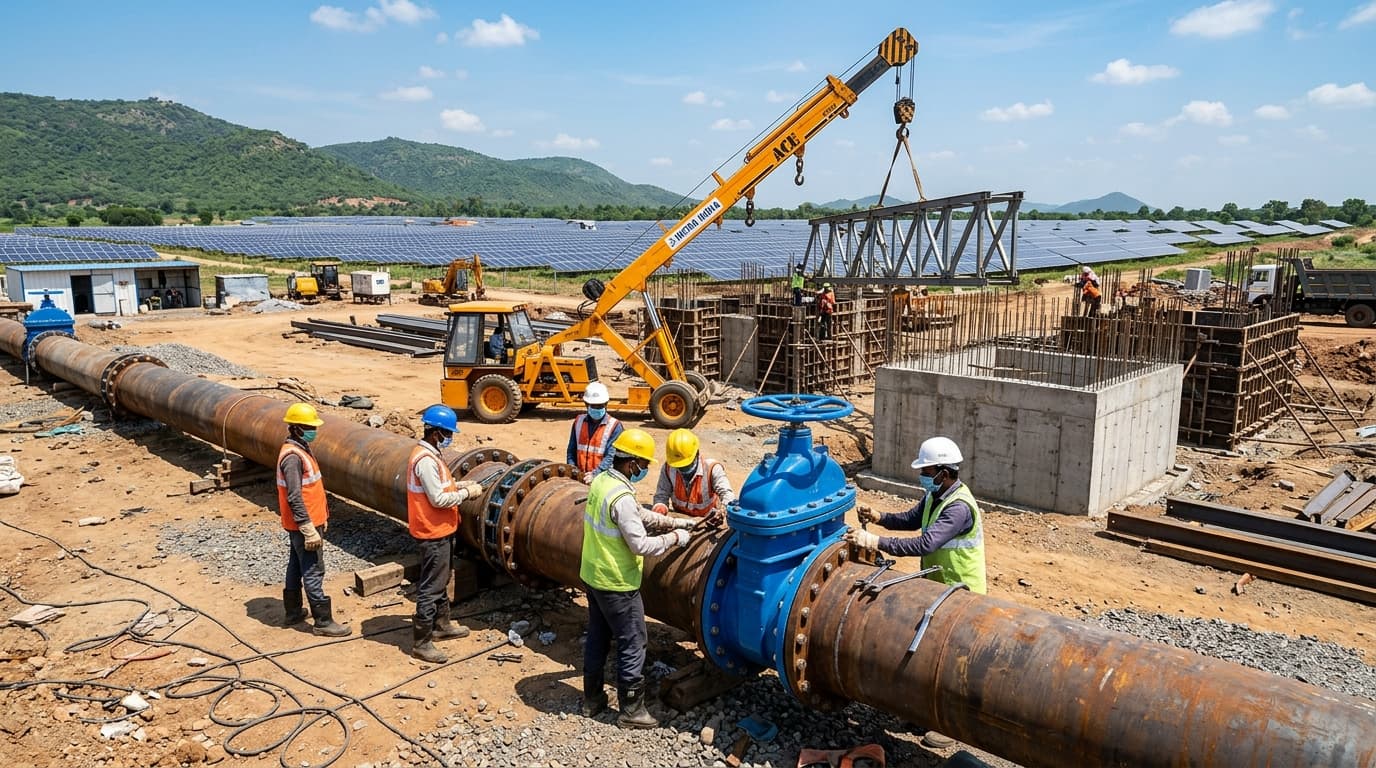
Representative application
Central vacuum-cleaning systems
Representative application
Process extraction
Representative application
Water and wastewater plant duties
Enquiry checklist
Specify the Duty Before Selection.
Share the available operating information so the package can be reviewed against the actual site requirement.
Send Product Requirements- 01
Required suction capacity and vacuum level
- 02
Gas composition and inlet filtration
- 03
Continuous or intermittent operation
- 04
Discharge, silencing and control requirements
Product details
Robust Design. Consistent Performance.
The final configuration is reviewed around the operating duty, handled medium, available utilities and installation interfaces.
- Twin-lobe positive-displacement arrangement
- Suction capacity matched to vacuum level
- Inlet filtration selected for the process
- Temperature and duty cycle reviewed
- Silencing and discharge options configurable
- Controls coordinated with the wider system
Let's talk
Send the duty details, quantity, delivery location and any available specification sheet for review.